

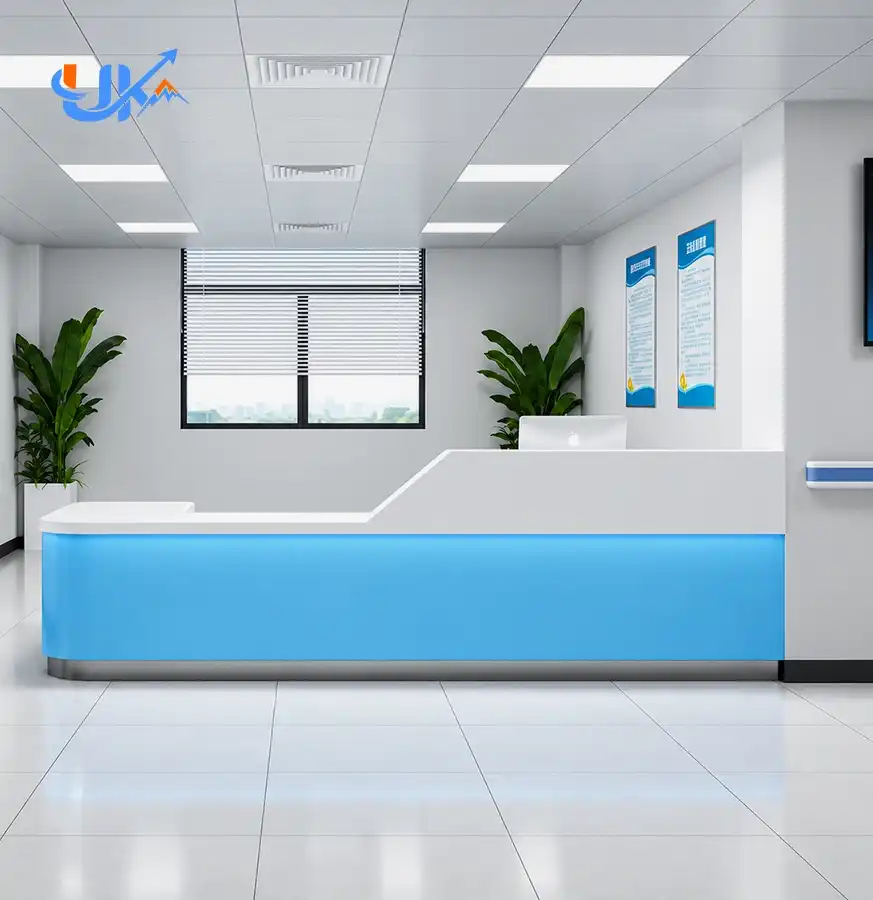
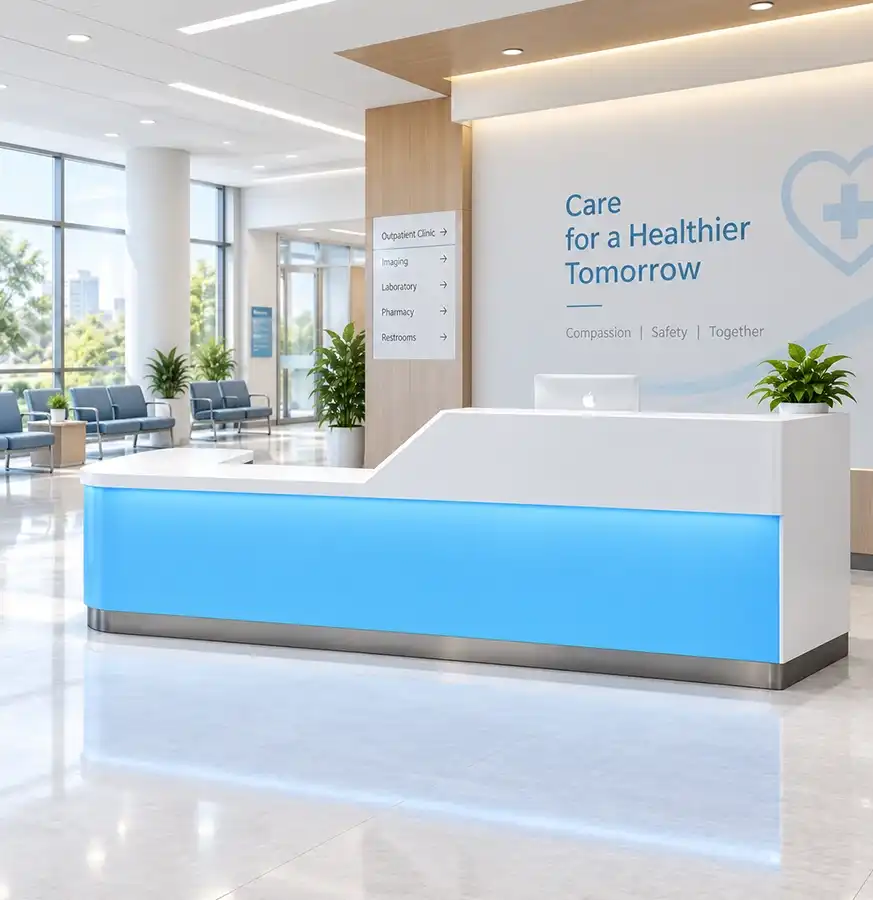
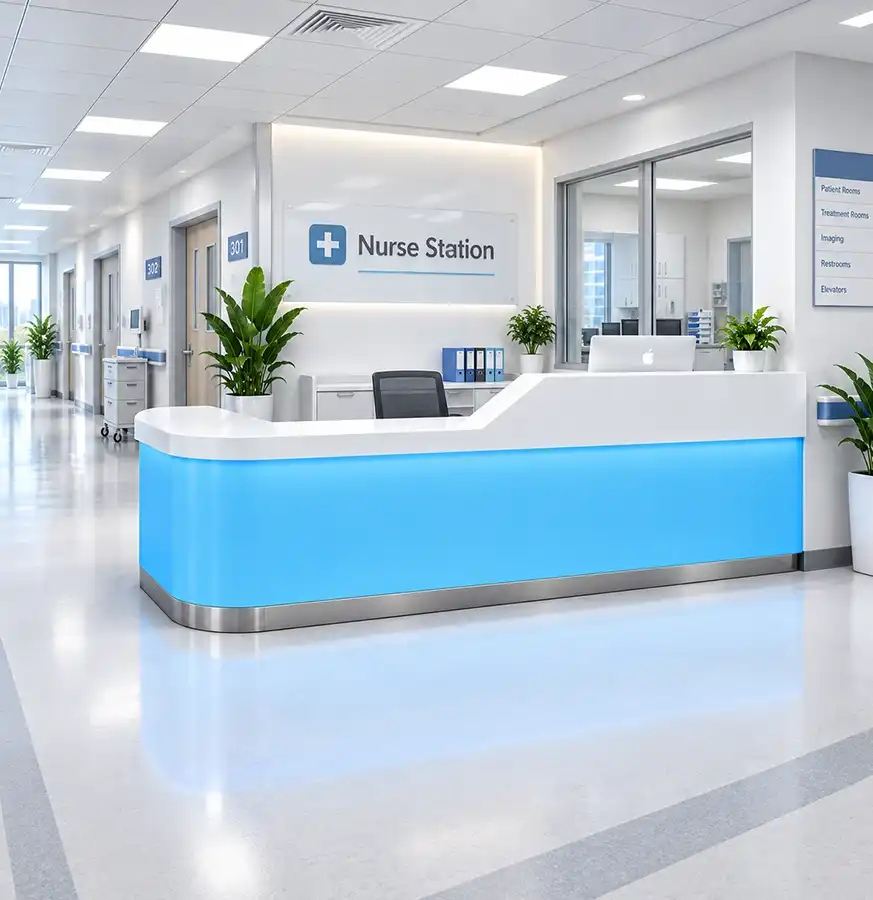
Reception Desk Clinic
Comfortable Operation: Humanized design improves staff working convenience
Neat Arrangement: Spacious compartments keep items clean and orderly
Clean Surface: Easy-wipe finish supports hygiene management
Practical Layout: Helps nurses and reception staff work more efficiently
Custom Solution: Available in customized size, color, and configuration
Quality Assurance: CE, ISO, and CQC qualified for project needs
- Product Description
Reception Desk Clinic Solutions | Medical-Grade Nurse Station for Healthcare Facilities
When healthcare facilities require a reliable and hygienic workstation, a Reception Desk Clinic becomes essential infrastructure. Luoyang Youken Laboratory Equipment Co., Ltd. manufactures medical-grade reception desks designed specifically for nursing stations, hospital reception areas, and clinical environments. We have a 30,000 square metre manufacturing facility and 100 skilled engineers to provide customised solutions meeting ISO, CE and CQC international quality requirements. Our solution has a sturdy cabinet structure, many compartments for organised storage, and easy-to-clean surfaces to meet rigorous hygiene requirements in pharmaceutical labs, medical facilities, and healthcare organisations.
Professional Medical Workstation Design
Your nursing staff deserves furniture that enhances daily workflow efficiency. Our product combines robust construction with humanized layout planning. The spacious compartments accommodate patient files, medical supplies, administrative tools, and electronic equipment systematically.
The smooth surface finish allows quick sanitization between patient interactions. This design consideration directly addresses infection control requirements in busy healthcare settings. The stable structure withstands continuous use throughout long shifts without compromising stability.


Technical Specifications of Reception Desk Clinic
| Parameter | Description |
|---|---|
| Material | Medical-grade panel with anti-bacterial coating |
| Dimensions | Fully customizable based on space requirements |
| Load Capacity | Heavy-duty construction supports equipment and supplies |
| Surface Finish | Easy-wipe, stain-resistant coating |
| Storage Configuration | Adjustable compartments, drawers, and cable management |
| Color Options | Customizable to match facility branding |
| Certification | CE, ISO, CQC qualified |
| Customization | Size, color, layout, and structure adaptable |
Core Advantages for Healthcare Environments
Furniture built exclusively for the medical industry has a positive impact on your clinical environment. The product has a sturdy build that will last through regular everyday activities without degeneration. Strong cabinet bodies are impact resistant and preserve structural integrity for years of use.
The proportions of the storage sections are practical. Medications, medical data, computer terminals and communication equipment may be organised neatly. This organised method cuts down on personnel fatigue and speeds up reaction times in emergencies.
The minimal maintenance finish helps to save operating expenses. A simple wipe down with basic medical grade disinfectants maintains surfaces clean and hygienically. This functionality is very useful for institutions that have significant patient numbers and need to be as time efficient as possible.
Flexible design choices enable you to set precise size to meet your welcome area. Whether you require more counter space for numerous workstations or compact designs for small floor plans, customisation is the perfect solution for maximising your space.

Multi-Industry Applications
Healthcare institutions across various sectors rely on properly designed reception stations. Pharmaceutical laboratories use our desks for sample logging and documentation management. Medical laboratories benefit from the chemical-resistant surfaces when handling specimen paperwork.
Educational medical facilities appreciate the durability during high-traffic training periods. Research and development laboratories incorporate these workstations into clinical trial coordination areas. Hospital operating room preparation zones use compact versions for pre-surgical documentation.
Clean room environments in GMP facilities require furniture that meets strict contamination control standards. Our Reception Desk Clinic satisfies these requirements through flush-mounted designs and non-porous surface materials that prevent particle accumulation.
Installation and Integration
Your facility infrastructure is 100% compatible with our modular infrastructure. The desk has built-in channels for electrical routeing for computer systems, phones and patient call devices. Cable management systems provide neat environments and allow for simple access for maintenance.
Before manufacture, the engineering team offers layout guidance. This allows the best location to be selected based on patient flow patterns, emergency access demands, and staff ergonomic considerations. Anchor points are selected for safe installation without interference with structural elements.
Weight distribution engineering prevents tipping when all drawers are opened simultaneously. This safety concern protects personnel and equipment when the facility is busy. Adjustable levelling feet make up for the uneven floors seen in older facilities.
Quality Assurance & Manufacturing Standards
We have strict quality control measures in our manufacturing process as per the worldwide requirements of healthcare furniture. Each product is load tested to mimic years of operating duress. Chemical resistance testing of surface coating using standard hospital disinfectants
The 30,000 square metre production base enables to fully regulate the production chain. Raw material inspection guaranties that only certified Medical Grade components are used in assembly. Finishing activities are not started until welding and joint integrity have been separately checked.
ISO-certified procedures govern every manufacturing stage from cutting to packaging. This systematic approach delivers consistent quality whether you order a single unit or equip an entire hospital network. SEFA and SGS certifications provide additional assurance for international procurement projects.

FAQ
Q:Are you a manufacturer or a trading company?
A:We are a professional manufacturer, supporting direct factory supply and customized project solutions.
Q:What is your minimum order quantity?
A:The MOQ depends on the product type and customization requirements. Trial orders and project sample orders are welcome.
Q:What is the production lead time?
A:The normal production time is approximately 20–53 days after the drawings, specifications, and deposit are confirmed. The exact lead time depends on order quantity and customization level.
Q:Do you support OEM and ODM services?
A:Yes. We support OEM and ODM cooperation, including customized dimensions, colors, branding, packaging, product structures, and project-based manufacturing.
Q:Can you manufacture according to our drawings?
A:Yes. We can manufacture according to your CAD drawings, product specifications, sample photos, or project requirements.
Contact Us
Ready to upgrade your clinical Reception Desk Clinic workstations? Reach out to our engineering team at ceo@ukenlab.com for customized solutions tailored to your facility requirements.
CUSTOMER REVIEWS
What Our Customers Say